
One of the UK’s sole manufacturers of gobos, Projected Image is helping manufacturers around the country to modernise their facilities and minimise downtime.
Now into its 27th year of business, Projected Image (est. 1999) is an industry leader in projected signage solutions. Originally starting out as a supplier of gobos to the live events and lighting industries, the company quickly made a name for itself in the reliability and high quality nature of its solutions, becoming one of the industry’s most trusted suppliers. Recognising the potential application and market for projected signage within the manufacturing and warehousing industries, however, the company has more recently ridden the wave of helping organisations to modernise their facilities and fully leverage the power of projected signage within. Let’s take a closer look.
To unpack Projected Image’s proposition, we must first respect the infancy of the projected signage market, particularly within the manufacturing sector. Although certainly a rapidly growing market, projected signage is still considered the figurative “new kid on the block”, with many being unaware of the strengths of projected signage or unsure if it can suit their use-case. As such, it’s worth briefly covering the benefits of projected signage itself, before then looking to what makes Projected Image stand out within that segment.
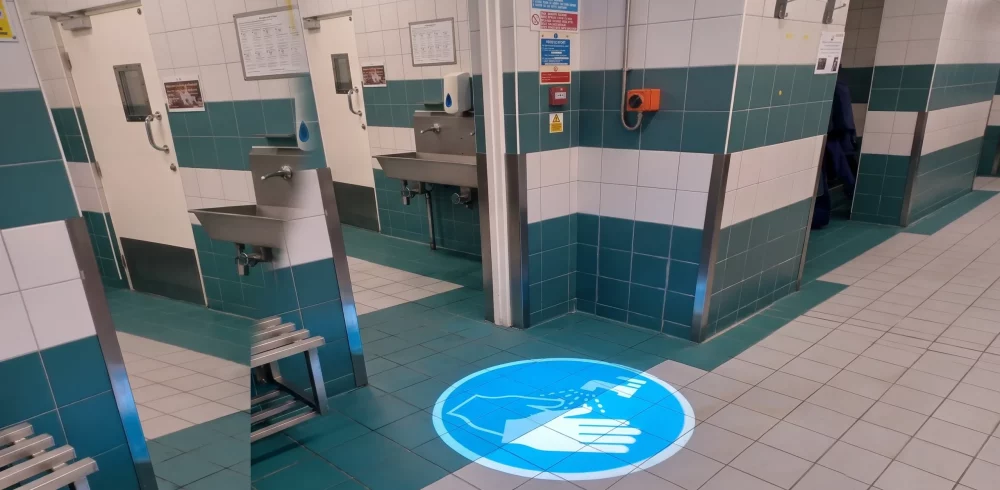
Starting with the fundamentals, projected signage incorporates the use of high-powered LED projectors to cast bright, safety-compliant signage directly onto surfaces where painted signage would traditionally be used. Used either to replace or enhance painted signage (as the two can complement one another in specific use-cases and layouts), projected signage is highly effective in displaying visible, compliant signage in high traffic areas where painted signage solutions are prone to rapid deterioration – especially due to the use of plant and heavy machinery. Moreover, projected signage carries all of the core compliance and benefits of traditional painted signage.
So, where projected signage shines is fundamentally in the application and maintenance of signage solutions. While traditional painted signage may require replacing multiple times per year (particularly in high traffic areas), LED projected signage offers a much more robust circa 50,000 hours of life (assuming 24/7 operation) and, moreover, upon the end of life for both product offerings, painted signage requires the specific cordoning off of areas for significant periods of time (effectively taking a space offline), while projected signage can be easily updated in as little as one hour with limited disruption to on-site operations.
Understandably, this offering presents a huge cost and productivity benefit for manufacturers, allowing for reduced disruption in operations and much simpler maintenance. Even on a raw cost basis, it can be estimated that projected signage solutions can outperform painted signage with a ROI of only a year (assuming high traffic location), making it an increasingly tempting alternative to manufacturers and warehouse owners.
“On average, areas with very heavy traffic such as forklifts or heavy machinery require the re-painting of signage twice per year,” explained Ian Spoors, Managing Director of Projected Image. “But once you’ve re-painted that signage twice, you’ve already saved money by doing it with a projector. These projectors are also LED, so they are lasting up to 50,000 hours, so you can have that signage installed and put, with it being as bright as the day you put it in until that LED eventually need replacing (a considerable amount of time).
“Considering when areas need to be shut down for re-painting also adds to that cost-factor (it can take 5-6 hours for the paint to be applied and dry). With a projector you can have an electrician come in to where you want the signage and it’s done in an hour instead.”
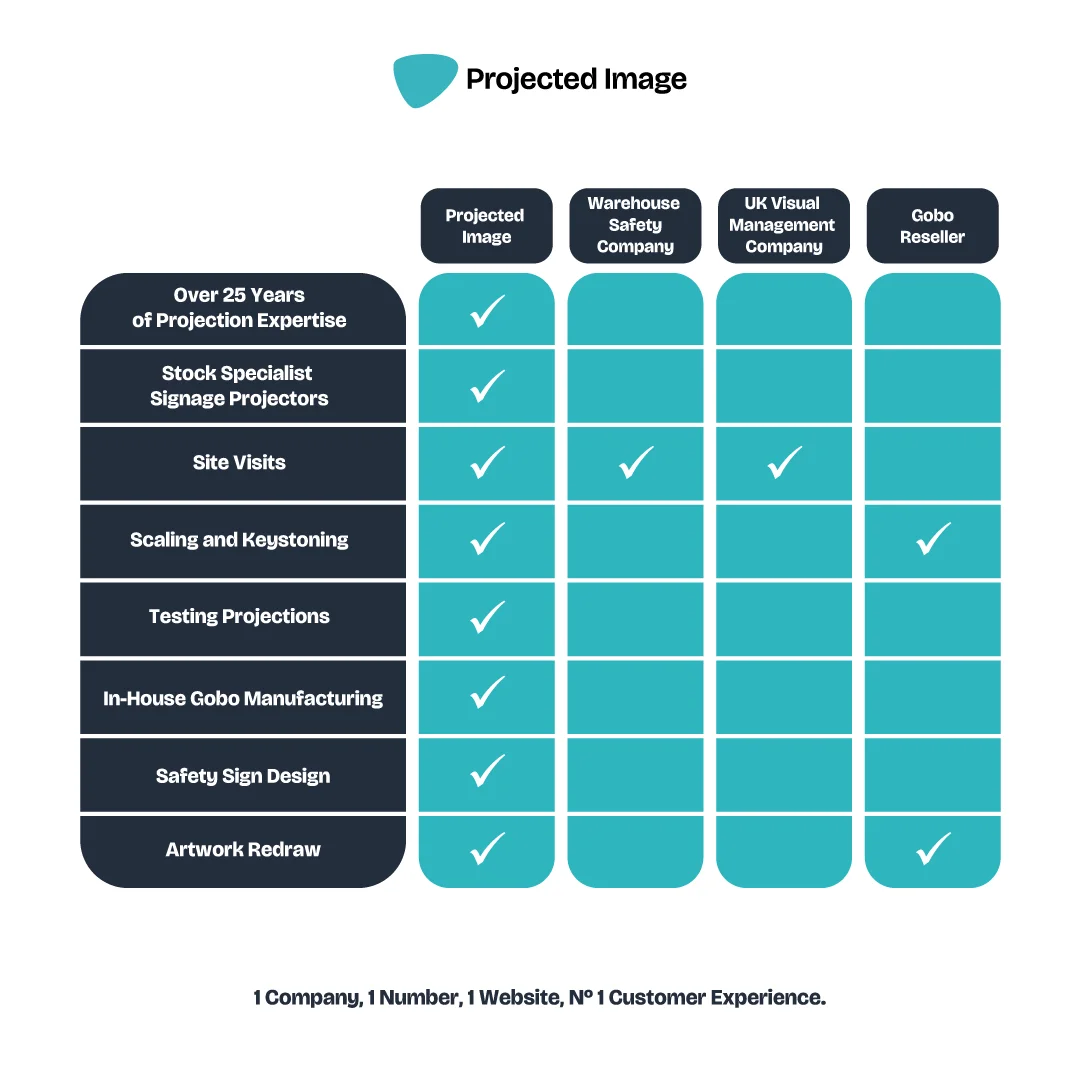
Now looking more closely at Projected Image exclusively, where the organisation stands out from its peers is in the sheer depth of expertise and capabilities that the company brings. Unlike many in the space, Projected Image manufactures all of its gobos in the UK with strict quality controls and offers a single-source solution for both gobos and the associated projector; this ultimately allows for a unified client experience where Projected Image can offer end-to-end assurance and tailor the manufacture of product around the individual needs of a client (particularly relevant in unique signage solutions or considering challenging locations and surfaces).
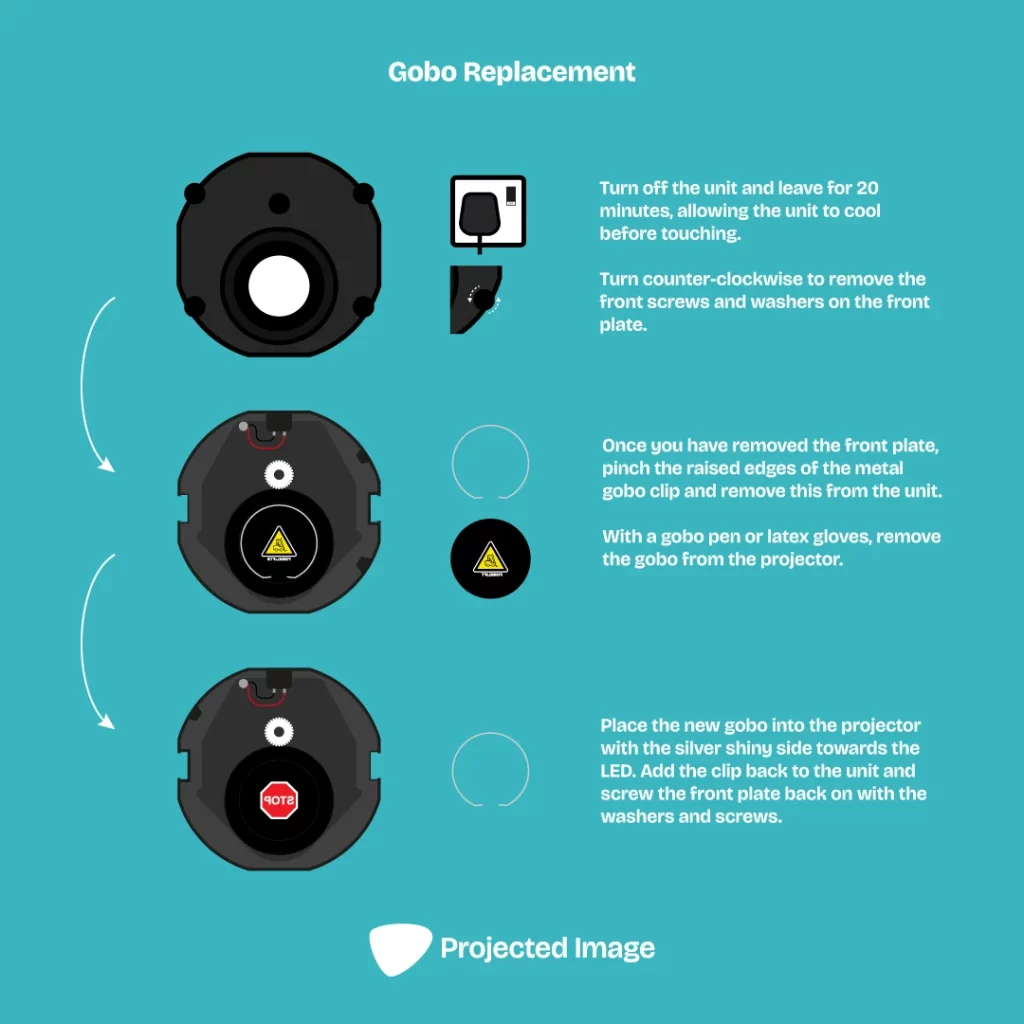
Furthermore, Projected Image is able to offer extensive added value in the form of industry leading expertise as to the installation and application of projected signage solutions. Recognising that no two factories or warehouses are the same, the organisation works alongside clients to identify their signage needs, propose solutions (even if this may include suggesting a traditional painted signage solution alongside), and ensure the correct lighting, roofing, and surface conditions for a client’s specific requirement. Ultimately, this coalesces to present a service which can guarantee a client’s intended requirement is met on-time, and within budget.
Nodding to the firm’s long-standing history in the industry and the expertise therefore available, Ian continued: “We have been doing this for 27 years so far. What you need from a relatively new product in this industry is that, firstly the product can fit the place perfectly (that is done in the manufacturing of the gobo, which can be scaled and adjusted for any angles you’re projecting onto), and secondly getting the projector into the right place (lighting is different in any warehouse you go into). To do that you need the right combination of experience and product, but there are hundreds of gobo projectors out there and most are not actually fit for a factory or warehouse.”
As a result, Projected Image is the partner of choice for many organisations now seeking to modernise their facilities, pairing the essential manufacturing capabilities with installation and maintenance expertise that guarantees client satisfaction. Also carrying stock of all of its projectors and able to manufacture gobos at a rapid speed, the company is able to offer a level of responsiveness that only adds to these relationships and makes Projected Image a critical partner in modernising factories and warehouses for the future.
Manufacturing & Engineering Magazine | The Home of Manufacturing Industry News